
Water resource recovery processes at Clarkson and G.E. Booth
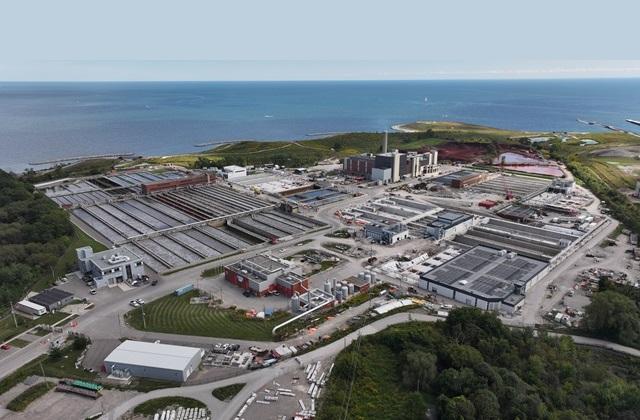
Clarkson and G.E. Booth are in Mississauga. Both facilities are located on – and discharge treated water back into – Lake Ontario.
Wastewater treatment facilities can emit odours because bacteria break down the waste in the water, and this natural process releases smells into the air.
Peel Region monitors and reduces wastewater odours through advanced technology, regular inspections, quick response, and facility upgrades.

Clarkson
Processes the wastewater from homes and businesses on the west side of Brampton and Mississauga.
Designed to treat an average flow of 350,000 m3 per day (350 ML per day).
G.E. Booth
Processes the wastewater from homes and businesses in Bolton, Caledon East, the east sides of Brampton and Mississauga, as well as some areas of York Region and the City of Toronto.
Designed to treat an average flow of 518,000 m3 per day (518 ML per day).
Preliminary treatment – headworks
Preliminary treatment removes coarse materials that could damage or clog downstream equipment and make treatment less efficient.
Wastewater from the collections system enters the recovery facility through the headworks. The headworks consists of mechanical screens, grit removal chambers and other associated equipment.
All wastewater flows through mechanical screens. These screens capture and remove materials such as rags, plastics, metals and wipes. The screened materials are washed and compacted before disposal.
The wastewater then flows through the grit removal chambers, where a vortex-type flow pattern makes grit settle to the bottom of the tank. Every so often, grit slurry pumps remove accumulated grit, which has excess water removed before disposal.
Primary treatment – anaerobic chamber
Primary clarifiers are large tanks. They slow the flow to allow readily settleable solids to sink to the bottom of the tank.
A sludge layer forms at the bottom of the tanks where sludge collection equipment sweeps it to the collection hoppers. Skimmers remove the surface scum layer, which consists of floating materials. The sludge and scum are then pumped to the biosolids facility for processing.
"Influent" is water that flows in, while "effluent" is water that flows out.
Primary effluent refers to flow that has undergone primary treatment (whereas primary influent is the flow entering the process). This treated primary effluent then flows by gravity to the secondary treatment phase.
Secondary treatment – activated sludge and collection hoppers
The conventional activated sludge process has 3 parts: biological reactors (aeration tanks), settling tanks (secondary clarifiers) and a solids recycling stream.
Aeration tanks are large tanks where dense populations of microorganisms consume both particles and dissolved substances.
Air is bubbled up from diffusers at the bottom of the tanks to provide oxygen to the microorganisms. This air also keeps the microorganisms in suspension.
Biomass is a mass or clump of organic matter that is used as a fuel. The combined biomass of the aeration tank is called mixed liquor. The mixed liquor flows by gravity to the secondary clarifiers.
Secondary clarifiers are large tanks. They also slow the flow to allow readily settleable solids to sink to the bottom of the tank.
These tanks provide dormant conditions to settle the biomass out from the water.
The settled biomass forms a sludge layer called activated sludge. Collection equipment sweeps activated sludge into collection hoppers. A portion of the activated sludge is returned to the aeration tanks (return activated sludge) and the remainder (waste activated sludge) is removed to the biosolids facility for processing.
The treated secondary effluent is then disinfected.
Tertiary treatment – phosphorus removal

Phosphorous removal in the treatment process is enhanced using ferrous chloride. Ferrous chloride helps phosphorous in the wastewater settle to the bottom of the clarifiers.
Disinfection and outfall
Secondary effluent is disinfected to destroy disease-causing organisms prior to the release of final effluent into the environment.
Chlorination using sodium hypochlorite is used for disinfection at the G.E. Booth and Clarkson WWRRP's.
Low-level chlorine can have toxic effects on aquatic environments, so chlorination is followed by decholorination using sodium bisulphite. Sodium hypochlorite and sodium bisulphite are added before and mid-way along the outfall pipe, respectively. This allows a sufficient retention time for the corresponding chemical reactions.
Final effluent is discharged to Lake Ontario through each facility's outfall pipes, which extend over a kilometer from shore. Effluent is released via a series of ports that diffuse the water over a large area.
Solids handling process
Solids handling at the G.E. Booth WWRRP involves thickening, dewatering, incineration and ash storage in onsite lagoons. Solids handling at the Clarkson WWRRP consists of thickening, dewatering, and anaerobic digestion, with the final dewatered biosolids trucked to the G.E. Booth WWRRP for incineration.
Thickening and dewatering processes
Thickening and dewatering processes are used to reduce the liquid content of sludge and biosolids for various reasons, including increasing treatment capacity, reducing haulage volume and providing a material suitable for incineration.
Dewatering provides a higher level of liquids removal. The liquids these processes remove are returned to the liquids treatment stream. Polymers are used to increase thickening and dewatering efficiency.
Anaerobic digestion
Anaerobic digestion is a sludge stabilization process that happens in a heated, mixed, oxygen-free tank.
The anerobic digestion process receives both primary sludge and thickened waste-activated sludge. Sludge is mixed and heated in the digesters to stay between 35°C – 37°C for proper bacteria activity.
Sludge heating happens by continually recirculating the sludge through external shell and tube heat exchangers. At the Clarkson WWRRP, biogas that is produced in this process is captured and used to generate heat and electricity by cogeneration unit (cogen).
Stabilized sludge is referred to as biosolids.
Biogas handling facilities and cogeneration unit (cogen)
At the Clarkson WWRRP, digester gas that is generated in the anaerobic digesters is collected and used as fuel for the cogeneration unit and the hot water boilers.
Cogen is an effective way of providing non-conventional renewable energy to generate electricity to the internal high voltage grid and generate heat to keep the digestion tanks warm.
Gas boosters maintain the digester gas supply to the storage gas bubble for the cogen and the boilers. Excess gas that isn't used at the boiler unit is flared.
Incineration
G.E. Booth WWRRP and Clarkson WWRRP biosolids are incinerated at the G.E. Booth WWRRP.
Combustion air is fed into the windbox at the base of the incinerator. Dewatered biosolids and, if necessary, supplementary fuel (fuel oil or natural gas) is pumped into the fluidized sand bed.
Water is evaporated, and most of the solids combustion is processed within the sand bed. Final combustion happens above the bed in the freeboard section with exhaust gases exiting between 700°C – 900°C.
Exhaust air is cleaned and cooled prior to release into the atmosphere. These emissions are constantly checked by a continuous emissions monitoring system (CEMS).
Ash lagoons
The ash slurry produced from the incineration process is pumped to ash lagoons for onsite storage.
Biofilters
Biofilters are an air treatment system used to remove odorous compounds, particularly hydrogen sulfide (H₂S), reduced sulfur compounds, ammonia, and other water-soluble volatile organic compounds (VOCs).
Odorous air is drawn into the biofilters by a fan. Inside the vessel, a specialized media provides a surface where naturally occurring microorganisms grow and form a biofilm. Final effluent (waste) from the treatment process is continuously trickled over the media to keep the biofilm active.
As the odorous air passes through the filter, odour-causing compounds dissolve into the liquid and are absorbed into the biofilm. The microorganisms then biologically oxidize these compounds, converting them into stable, non-odorous by-products before the treated air is released to the atmosphere.
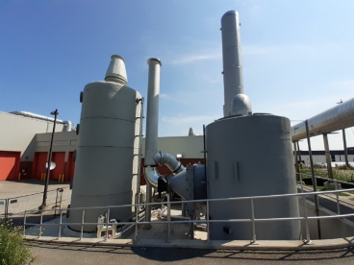
Biotrickling filter at G.E. Booth Wastewater Resource Recovery Facility
Granular Activated Carbon (GAC)
Granular Activated Carbon (GAC) is an odour control technology that removes odorous compounds from air through a process called adsorption. GAC is commonly used to treat air containing hydrogen sulfide (H₂S), reduced sulfur compounds, volatile organic compounds (VOCs), and other trace odour-causing contaminants.
Odorous air from the headworks facility and conveyance piping to primary and secondary treatment processes is drawn through vessels containing specially treated activated carbon. The activated carbon has an extremely large internal surface area with millions of microscopic pores that attract and capture odour-causing compounds as the air passes through the activated carbon bed (the layer of carbon granules inside the treatment vessel).
The treated air is then safely discharged to the atmosphere. Over time, the carbon becomes exhausted as its adsorption capacity is used up and must be replaced to maintain odour removal performance.
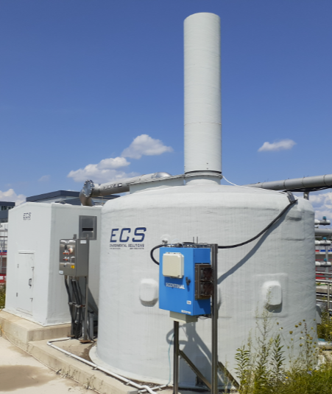
Granular Activated Carbon systems at G.E. Booth Wastewater Resource Recovery Facility (Plants 1 and 2)
Incinerator combustion air odour control
As part of the wastewater treatment process, odorous air from certain facility areas is collected and used as combustion air for the facility's incinerators. Rather than being released to the atmosphere, this air is drawn into the incinerators where it is exposed to the high temperatures required for sludge incineration.
The intense heat in the incinerators destroys odour-causing compounds, including hydrogen sulfide (H₂S), volatile organic compounds (VOCs), and other reduced sulfur compounds. This process provides effective odour control while also supplying air required for combustion.
By directing odorous air to the incinerators, the facility reduces odour emissions and makes efficient use of existing treatment infrastructure, helping to minimize impacts on the surrounding community.
Wet chemical scrubber
A sodium hydroxide wet chemical scrubber is an air treatment system designed to remove odours and harmful gases before they are released into the atmosphere. As contaminated air passes through the scrubber, it comes in contact with a recirculating sodium hydroxide solution that neutralizes odorous and acidic compounds, converting them into stable substances that can be safely managed within the system.
Sodium hydroxide scrubbers are particularly effective at controlling hydrogen sulphide (H₂S) odours.
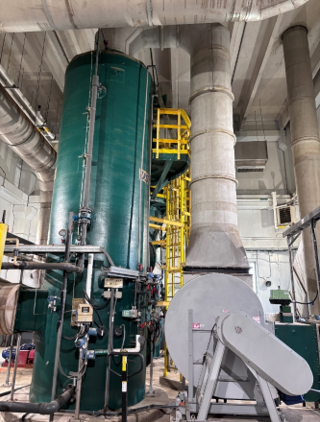
Wet chemical scrubber at Clarkson Wastewater Treatment Plant